What are you looking for?
Buying too little exhaust wrap can leave a header unfinished. Buying far too much adds unnecessary cost, particularly when the material is being specified for repeat OEM production.
The amount of exhaust wrap required is determined mainly by four dimensions:
exhaust pipe outside diameter;
total pipe length;
exhaust wrap width;
installation overlap.
Pipe bends, collectors, branches and installation waste can increase actual consumption, so a calculated value should be treated as the minimum theoretical requirement rather than an exact purchasing quantity.
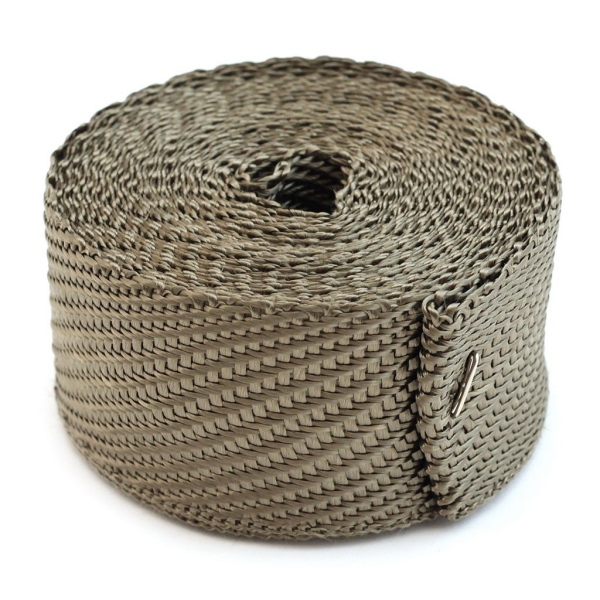
BSTFLEX manufactures exhaust and header heat wrap in multiple materials, widths and roll configurations for automotive, motorcycle, racing, diesel and industrial exhaust systems.
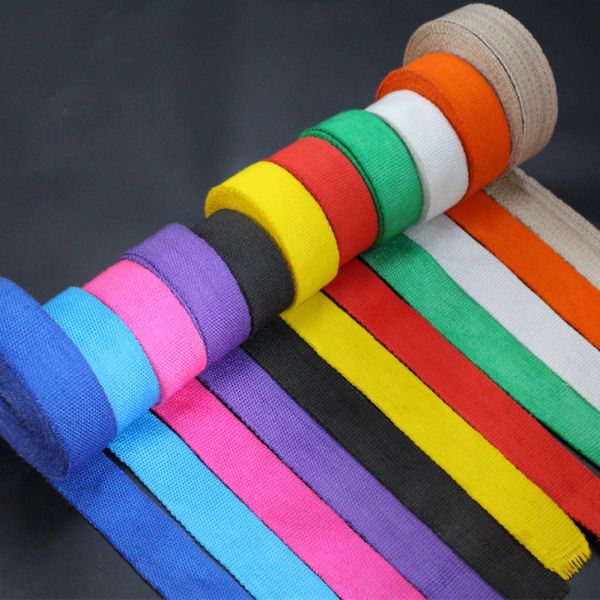
For a straight round exhaust pipe, wrap consumption can be estimated using a helical-wrap calculation.
Use:
D = pipe outside diameter
W = wrap width
O = overlap
P = effective advance per turn
where:
P = W − O
The approximate length multiplier is:
Wrap Length Multiplier = √[(πD)² + P²] ÷ P
Then:
Required Exhaust Wrap Length = Pipe Length × Wrap Length Multiplier
Use the same unit for pipe diameter, wrap width and overlap.
For example, if D, W and O are entered in inches, the multiplier can still be applied directly to pipe length in feet.
This calculation estimates the material required for a straight cylindrical pipe.
It does not automatically account for:
bends;
collectors;
flanges;
branches;
uneven overlap;
starting and finishing allowance;
installation waste.
Commercial exhaust-wrap calculators use the same basic inputs. DEI, for example, asks for pipe outside diameter, pipe length, wrap width and overlap, with 0.25 inch shown as its recommended default overlap. DEI also warns that its calculator does not account for bends.
Assume:
Pipe OD: 2 inches
Pipe length: 3 ft
Wrap width: 2 inches
Overlap: 0.25 inch
Effective advance:
2.00 − 0.25 = 1.75 inches
Circumference of the pipe:
π × 2 = approximately 6.28 inches
One helical turn therefore uses slightly more material than the pipe circumference because the tape travels diagonally along the pipe.
Using the formula above, the wrap-length multiplier is approximately:
3.73
Therefore:
3 ft × 3.73 = approximately 11.2 ft of wrap
That is the theoretical requirement for a straight section.
For a real exhaust installation, additional material should be allowed for bends, starting and finishing points and installation variation.
The following examples assume:
2 inch wide exhaust wrap;
0.25 inch overlap;
3 ft of straight exhaust pipe.
| Pipe Outside Diameter | Approx. Wrap Required |
|---|---|
| 1.5 in | 8.6 ft |
| 2.0 in | 11.2 ft |
| 2.25 in | 12.5 ft |
| 2.5 in | 13.8 ft |
| 3.0 in | 16.4 ft |
These figures are theoretical straight-pipe estimates.
Actual header and manifold installations normally use more material.
Larger exhaust pipes require more material because every turn must cover a greater circumference.
A 3-inch exhaust pipe has roughly twice the circumference of a 1.5-inch pipe.
This means two exhaust systems with the same pipe length can require very different amounts of wrap.
Pipe outside diameter should therefore always be measured before ordering material.
Do not estimate wrap quantity based only on:
engine size;
vehicle model;
horsepower;
number of cylinders.
The actual tubing dimensions matter more.
Overlap determines how far the wrap advances along the pipe with each turn.
More overlap means:
greater material consumption;
more insulation thickness;
slower axial coverage.
Less overlap means:
less material consumption;
thinner effective coverage;
greater risk of inconsistent gaps if installation is poor.
For example, with a 2-inch-wide wrap:
0.25-inch overlap
leaves:
1.75 inches of effective forward coverage per turn.
If overlap is increased, effective forward movement decreases and more wrap is required.
Current DEI calculators use 0.25 inch as a recommended default value, but that should not be treated as a universal requirement for every wrap manufacturer or application.
Always follow the installation instructions for the specific product being used.
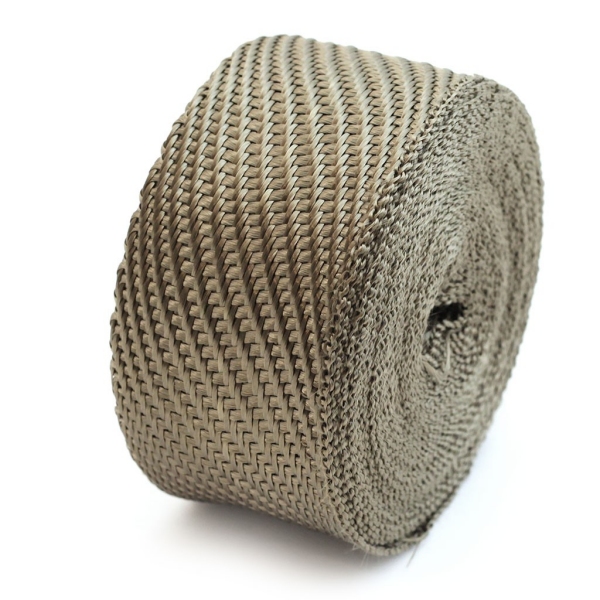
Wrap width has a significant effect on the length required.
A 1-inch wrap makes more turns over the same pipe length.
It is therefore particularly suitable for:
tight header bends;
small-diameter tubing;
motorcycle exhaust pipes;
complex manifolds;
closely spaced primary tubes.
However, more linear feet of tape will usually be required than with a wider wrap.
A 2-inch wrap advances farther along the pipe with each turn.
It is generally suitable for:
automotive headers;
downpipes;
medium-diameter exhaust tubing;
longer straight pipe sections;
faster installation.
Two-inch fiberglass and titanium-style wraps are common commercial sizes. DEI currently sells multiple 2-inch wrap configurations in 15-, 25-, 50- and 100-ft lengths.
The correct choice should depend on pipe geometry rather than simply selecting the widest tape available.
Consider the same 2-inch OD pipe.
If a narrow 1-inch wrap is installed with proportional overlap, the effective axial advance per turn is smaller than with a 2-inch wrap.
This means more revolutions are required to cover the same pipe length.
The narrower wrap can still be the better choice if the pipe includes multiple tight bends.
This is why exhaust header wrap selection involves a balance between:
material consumption;
installation speed;
conformability;
pipe geometry.
Headers are more difficult to calculate than straight pipe.
A tubular header may contain:
several primary tubes;
tight bends;
collectors;
merging sections;
flanges;
unequal tube lengths.
The correct method is to measure each primary tube separately.
For a four-cylinder header:
Measure each primary tube from flange to collector.
Record the OD of each tube.
Calculate wrap usage for each tube.
Add the collector if it will also be wrapped.
Add extra material for bends and finishing points.
Do not simply measure the total physical width of the header assembly.
Each tube must be treated as its own wrapped cylinder.
A V8 header set can consume substantially more material because eight primary tubes must be wrapped.
Some complete commercial kits therefore contain around 100 ft of 2-inch wrap.
For example, DEI currently markets automotive header wrap kits containing 100 ft of 2-inch glass-fiber wrap together with related installation accessories.
That does not mean every V8 requires exactly 100 ft.
Actual usage depends on:
primary tube length;
tube diameter;
overlap;
whether the collectors are wrapped;
header geometry.
For production applications, measuring the actual header remains more reliable than using engine configuration alone.
Motorcycles frequently use:
smaller pipe diameters;
tighter bends;
shorter overall exhaust lengths.
This often makes 1-inch or 2-inch wrap appropriate.
A motorcycle with two short header tubes may require much less material than an automotive multi-primary header.
DEI currently offers a motorcycle exhaust kit with 30 ft of 2-inch glass-fiber wrap, illustrating the shorter roll lengths commonly used in this application.
Again, the kit size should not be treated as a universal requirement.
Measure the actual motorcycle exhaust before ordering.
Turbo downpipes tend to be:
larger in diameter;
relatively short;
exposed to severe temperatures;
located close to sensitive engine-bay components.
The required wrap length can usually be calculated from the downpipe OD and centerline length.
However, downpipes often contain several bends.
Therefore the theoretical straight-pipe result should be increased with a practical installation allowance.
Material selection is also important.
For higher-temperature turbo systems, buyers may need to compare fiberglass with basalt or high-silica wrap rather than choosing material based only on roll length.
See Titanium Exhaust Wrap: Material, Temperature and Applications for basalt-based higher-temperature applications.
Tubular manifolds can be calculated similarly to headers.
Cast manifolds are more difficult because the surface may not form a consistent round tube.
If the component has:
irregular cast shapes;
very short branches;
complex flanges;
limited access;
a removable insulation blanket or formed heat shield may be more appropriate than spiral wrap.
The calculator in this guide is intended primarily for round exhaust tubing.
Yes.
A bend changes the effective path of the tape.
The outside radius requires more material than the inside radius, and the installer may need to adjust the overlap to keep the wrap smooth.
Commercial calculators commonly warn that their results do not account for bends. DEI explicitly states that bends will consume additional material beyond its calculated straight-pipe estimate.
For a complex exhaust system, it is better to purchase a sensible reserve rather than ordering exactly the theoretical result.
Additional material may also be required for:
The beginning and end of the wrap may require additional turns for secure fastening.
Collectors can change diameter quickly, increasing material use.
Formed and welded exhaust components may not maintain a perfectly constant diameter.
A section may occasionally need to be removed and rewrapped.
For OEM production, a small allowance may help prevent line stoppage caused by minor variation in installation.
Choose roll length from calculated consumption rather than visual estimation.
Typically appropriate for:
short exhaust sections;
smaller motorcycle systems;
individual downpipes;
single components.
Useful for:
longer motorcycle exhaust systems;
automotive headers;
several individual pipe sections.
Useful for:
multi-primary header systems;
larger jobs;
workshops;
OEM or repetitive installations.
Many current manufacturers offer these roll sizes. DEI, for example, lists multiple titanium-style exhaust-wrap products in 15-, 25-, 50- and 100-ft configurations.
BSTFLEX can also supply custom roll lengths for OEM and distributor projects where standard retail lengths create unnecessary joints or packaging waste.
The same calculation works with metric dimensions.
Use:
pipe diameter in millimeters;
wrap width in millimeters;
overlap in millimeters.
The multiplier remains dimensionless.
Then multiply it by the pipe length in meters to obtain an approximate wrap length in meters.
For example:
50 mm pipe OD;
50 mm wrap width;
6 mm overlap.
Effective advance:
50 − 6 = 44 mm
The calculation can then be applied in exactly the same way as the inch-based method.
This is particularly useful for industrial and OEM projects specified in:
25 mm wrap;
50 mm wrap;
metric exhaust tubing;
meter-length rolls.
For repeat manufacturing, BSTFLEX recommends recording the following information:
| Required Input | Example |
|---|---|
| Pipe OD | 50 mm |
| Pipe length | 1.2 m |
| Wrap width | 50 mm |
| Required overlap | 6 mm |
| Number of pipes | 4 |
| Number of bends | 6 |
| Wrap material | Fiberglass / Basalt / Silica |
| Production quantity | 500 assemblies |
This makes it possible to estimate both:
material consumption per assembly;
total roll requirement for the production order.
Retail roll sizes are not always efficient for manufacturing.
Suppose one finished exhaust component requires approximately 7.5 m of wrap.
Using a standard 10 m retail roll may leave significant unused material on every assembly.
For an OEM order, it may be more efficient to specify:
custom roll lengths;
master rolls;
pre-cut lengths;
kit packaging.
BSTFLEX can develop roll configurations around actual production consumption rather than forcing industrial customers to use consumer packaging formats.
The geometric calculation is essentially the same for:
fiberglass exhaust wrap;
basalt exhaust wrap;
titanium-style exhaust wrap;
silica exhaust wrap.
However, the finished material may differ in:
thickness;
flexibility;
weave;
stretch;
installation behavior.
Therefore calculated consumption should still be verified during prototype installation before finalizing a large production order.
For material selection, see the Exhaust Wrap Complete Guide and the complete BSTFLEX Exhaust and Header Heat Wrap range.
Calculating tape length is only part of the installation.
The wrap must also be secured.
Typical options include:
stainless steel locking ties;
stainless steel wire;
metal clamps;
purpose-designed bands.
Commercial exhaust wrap kits commonly include stainless steel ties together with the wrap. DEI, for example, packages locking ties with several of its header and exhaust wrap kits.
For OEM projects, wrap and fixing hardware can be specified as one packaged kit.
Before requesting a quotation, confirm:
Pipe outside diameter
Total pipe length
Number of pipes
Number of bends
Wrap width
Required overlap
Material
Temperature requirement
Roll length preference
Color
Required fasteners
Total quantity
Packaging format
If the exhaust geometry is complex, provide:
drawing;
CAD dimensions;
photographs;
sample part.
This allows material consumption to be estimated more accurately.
BSTFLEX manufactures exhaust thermal protection materials for automotive, motorcycle, motorsport, diesel and industrial applications.
Supply options can include:
1-inch exhaust wrap;
2-inch exhaust wrap;
25 mm exhaust wrap;
50 mm exhaust wrap;
custom widths;
custom roll lengths;
bulk master rolls;
pre-cut lengths;
stainless-steel fixing ties;
private-label exhaust wrap kits;
OEM packaging.
For fiberglass material selection, see Fiberglass Exhaust Wrap for Headers and Exhaust Pipes.
For all available material families, visit the BSTFLEX Exhaust and Header Heat Wrap category.
Measure the exhaust pipe outside diameter and length, then select the wrap width and required overlap. Use these values to calculate how much material is needed for each helical turn and the total number of turns along the pipe.
Yes. A larger pipe has a larger circumference, so every turn consumes more tape.
Yes. More overlap reduces the distance the wrap advances along the pipe with each turn, increasing total material consumption.
One-inch wrap is easier to install around tight bends and small pipes. Two-inch wrap generally installs faster on larger or straighter pipes.
Bends require more material than the straight-pipe calculation predicts. The exact amount depends on bend radius, pipe diameter, overlap and installer technique, so complex systems should include additional material allowance.
Measure each header primary tube separately and calculate the wrap requirement for every tube. Add the collector and additional allowance for bends and finishing points.
Yes. The same basic geometric calculation can be used for fiberglass, basalt/titanium-style and silica exhaust wrap, although different material constructions may behave differently during installation.
Yes. OEM and distributor orders can be configured around custom widths, custom roll lengths, bulk rolls, pre-cut lengths and private-label packaging.
No.10, Chuangxin North Road, Nanshan Park, Ningguo Economic and Technological Development Zone, Ningguo City, Anhui Province, China
Tel/Whatsapp : 0086-15856303740
Email : sales@bstbraidedsleeve.com
Skype : vanesa-cheng